Get in touch with Cenwan Machine Company
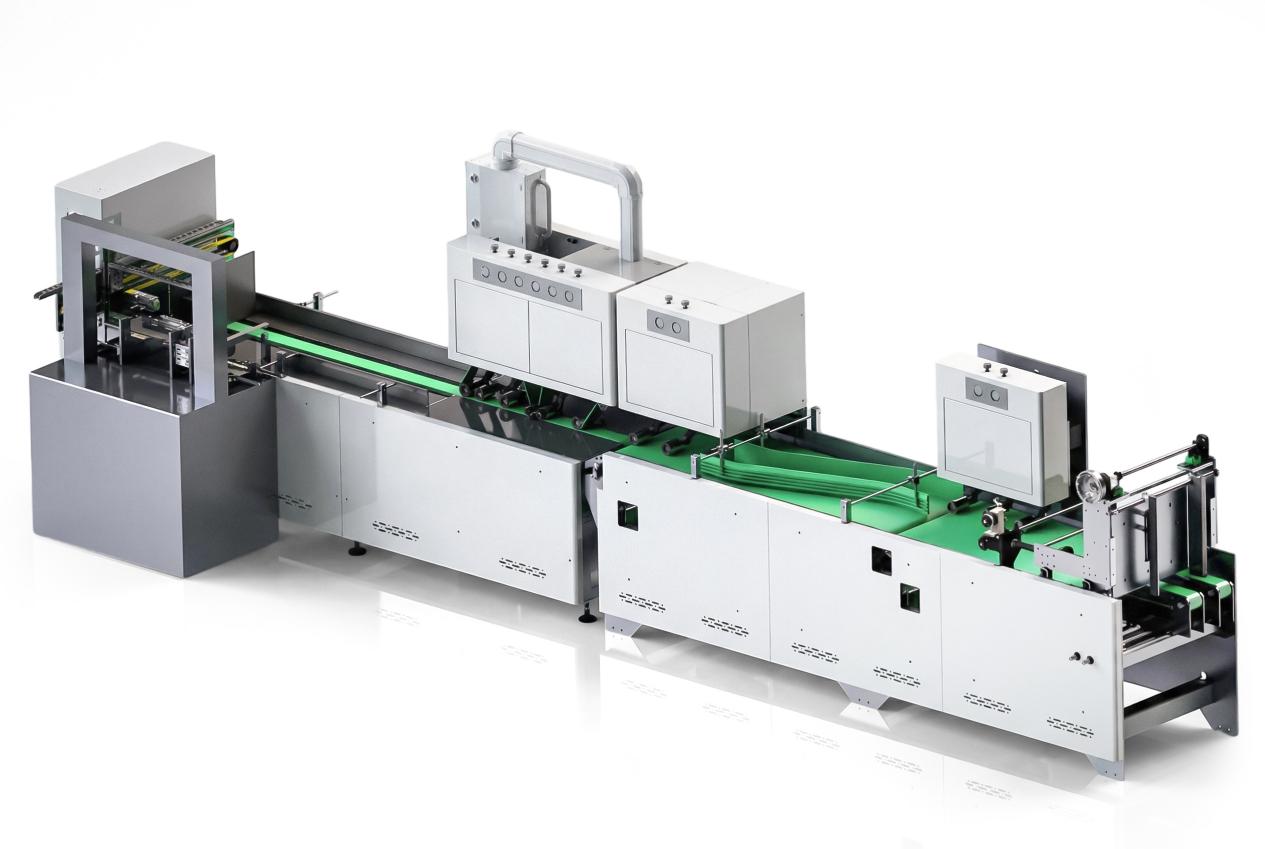
Fully Automatic Carton Counting, Stacking & Strapping Machine
For straight-line corrugated box production
Cenwan’s fully automatic carton counting stacking and strapping machine takes the shingled stream off your corrugated box folder gluer, counts it, stacks each count and ties it with PP strap. Tail-end automation takes counting, stacking and strapping out of hand work at your delivery end, and each strapped bundle leaves the machine as one closed package, ready for the pallet. The rated packing speed is 18,000–30,000 pcs/h; the rate you reach depends on box length, count per bundle and your folder gluer’s delivery.
Send Your Box Size for a Quote
Quotations are returned within 48 hours.
Counting, Stacking and Strapping Machine at a Glance
Four Patented Mechanisms of the Counting and Stacking Machine
The machine runs four patented mechanisms in sequence, and a PP strapping unit ties each finished stack. A full servo configuration with Inovance servo drives and an Inovance PLC runs the whole operation, and your operator sets the count per bundle on the Flexem HMI control panel.
Two-Stage Paper Feeding
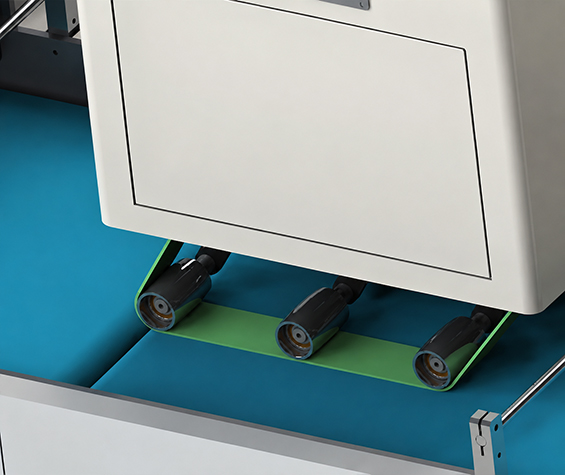
Boxes from your folder gluer pass through a two-stage feeder. The upper and lower belts have a speed differential. Boxes that may be overlapping are pulled apart before they reach the counting roller. This is the first defence against double counts.
Polling Counting with a Laser Displacement Sensor
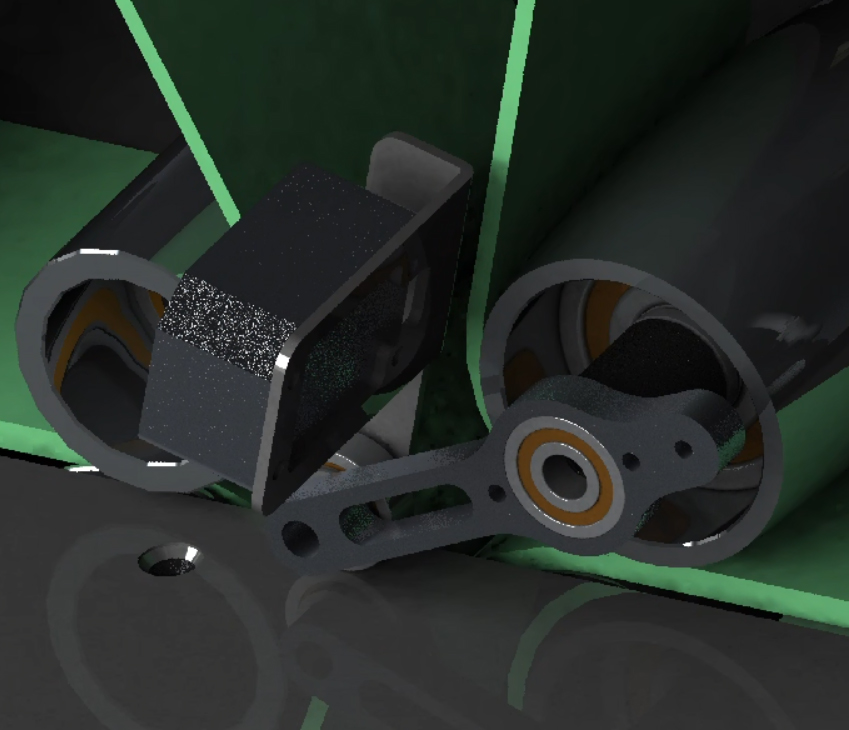
A roller rides across the surface of the shingled boxes. A laser displacement sensor tracks the roller’s rise and fall and counts the peaks and valleys the boxes form, one box per cycle. Laser triangulation measures distance from where the reflected spot lands on a position-sensitive detector.3
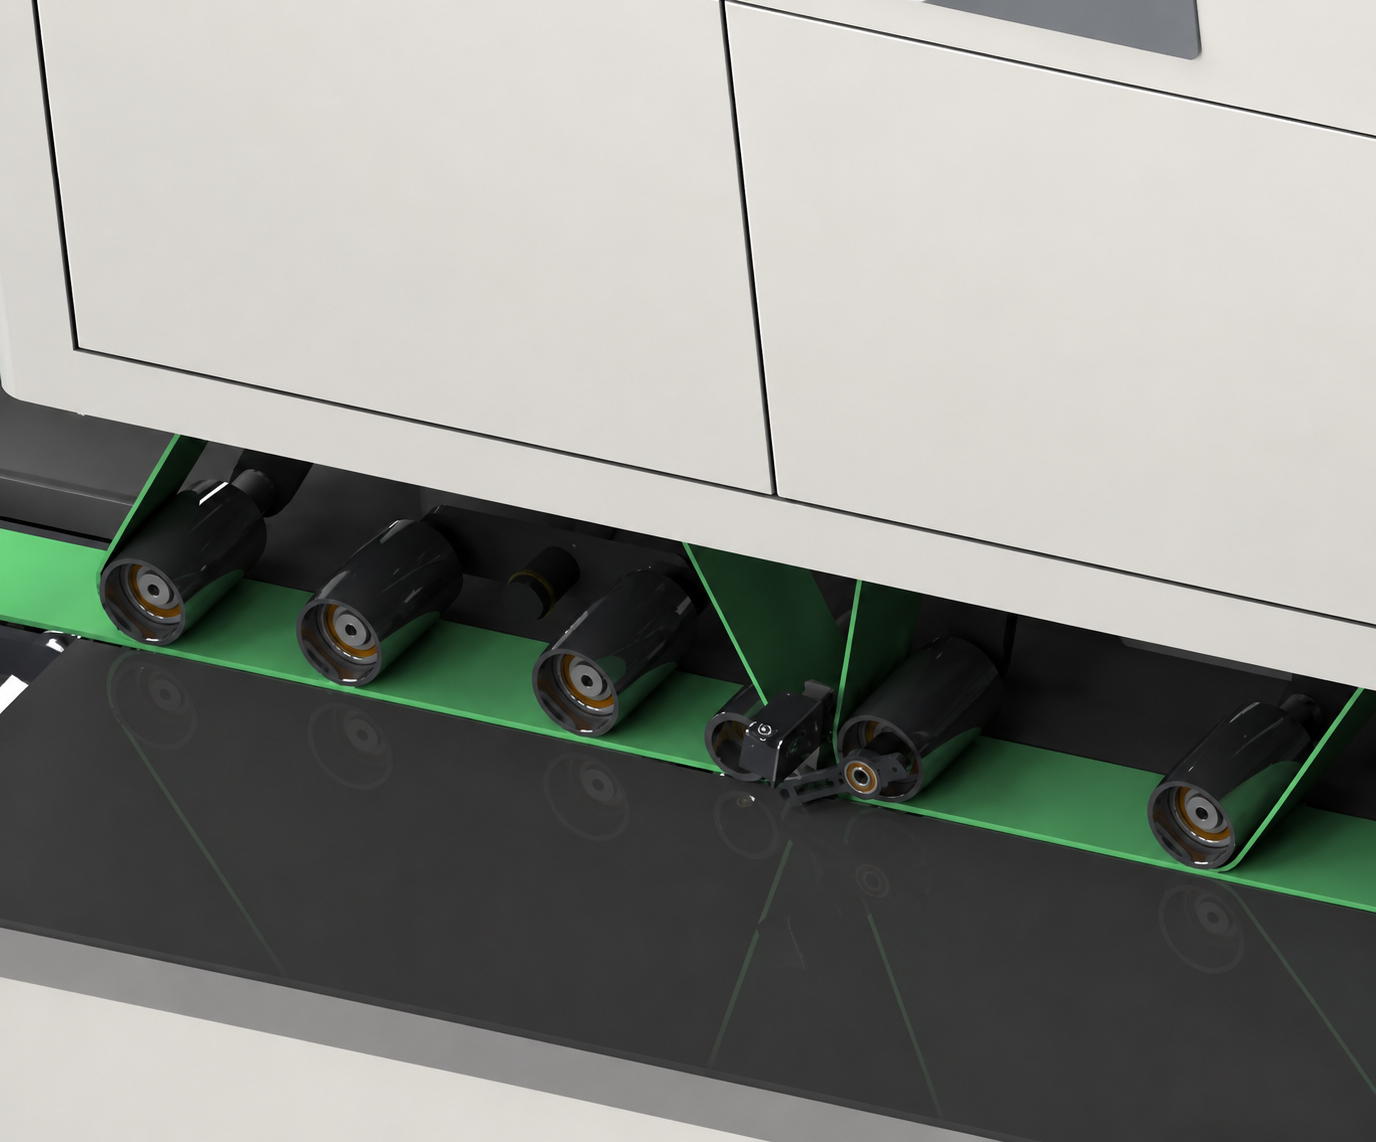
Servo Paper Separation
Once the set count is reached, the counting belt stops. The separation of the counted boxes from the next boxes is done by two belt assemblies with a pressure differential, under servo control.
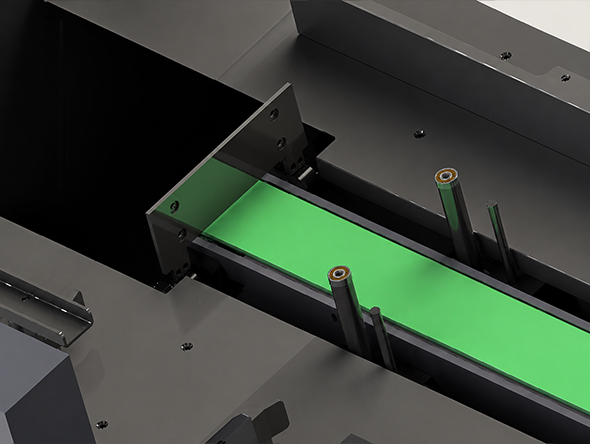
Carton Stacker Section: Pusher Rod and Flip Plate
Shingled boxes are stood up by a pusher rod and a flip plate and transferred to the strapping unit. The stack is built horizontally up to 550 mm uncompressed, or vertically up to 400 mm. The mode is set to your box size range at quotation.
PP Strapping Unit
The strapping process runs automatically, from strap feeding through tensioning, sealing and cutting: the unit feeds PP strap around the stack, tensions it, seals the joint, cuts the strap and releases the bundle.
It runs polypropylene strapping (PP strap), the material ASTM D3950 lists as Type II strapping: extruded, oriented polypropylene.1
A tighter strap does not always make a better bundle. Too much tension crushes carton corners and cuts into the board edge.
How the Machine Prevents Short or Double Counts
For a simple counter, counting an overlapped stream is accurate as long as item thickness and overlap are constant; if overlap varies, miscounts can easily occur, and creases and bulges also increase the errors.5 The feed matters because the roller counts the height profile of the stream. The two-stage belt speed differential separates the boxes that are overlapped prior to being read by the roller.
The counting belt comes to a stop at the set count and the servo separation parts the finished count from the next boxes.
Warped board, open flaps and glue that has not set change the profile the roller reads, so tell us your flute and board condition with your box sizes.
The count check, stack height, strapping and run length are acceptance criteria agreed in your contract before the factory acceptance test.
“Send us the smallest and the largest box you run and the count your customers order. Those two answers decide horizontal or vertical stacking before anything else goes into the quotation.”
Cenwan Application Engineering Team
Corrugated Board Grades and Box Size Definitions
The machine counts, stacks and straps corrugated straight-line boxes in B, C, E, BE, N and F flute. These are the glued, flattened corrugated cardboard boxes you manufacture on a carton production line, as they leave a straight-line folder gluer with a single glued joint.
| Flute Grade | Board Structure | What to send with your enquiry |
|---|---|---|
| B flute | Single wall | Flattened box size range and board caliper |
| C flute | Single wall | Flattened box size range and board caliper |
| E flute | Single wall, fine flute | Flattened box size range and board caliper |
| BE flute | Double wall (B and E) | Flattened box size range, board caliper and count per bundle |
| N flute | Micro flute | Flattened box size range, board caliper and count per bundle |
| F flute | Micro flute | Flattened box size range, board caliper and count per bundle |
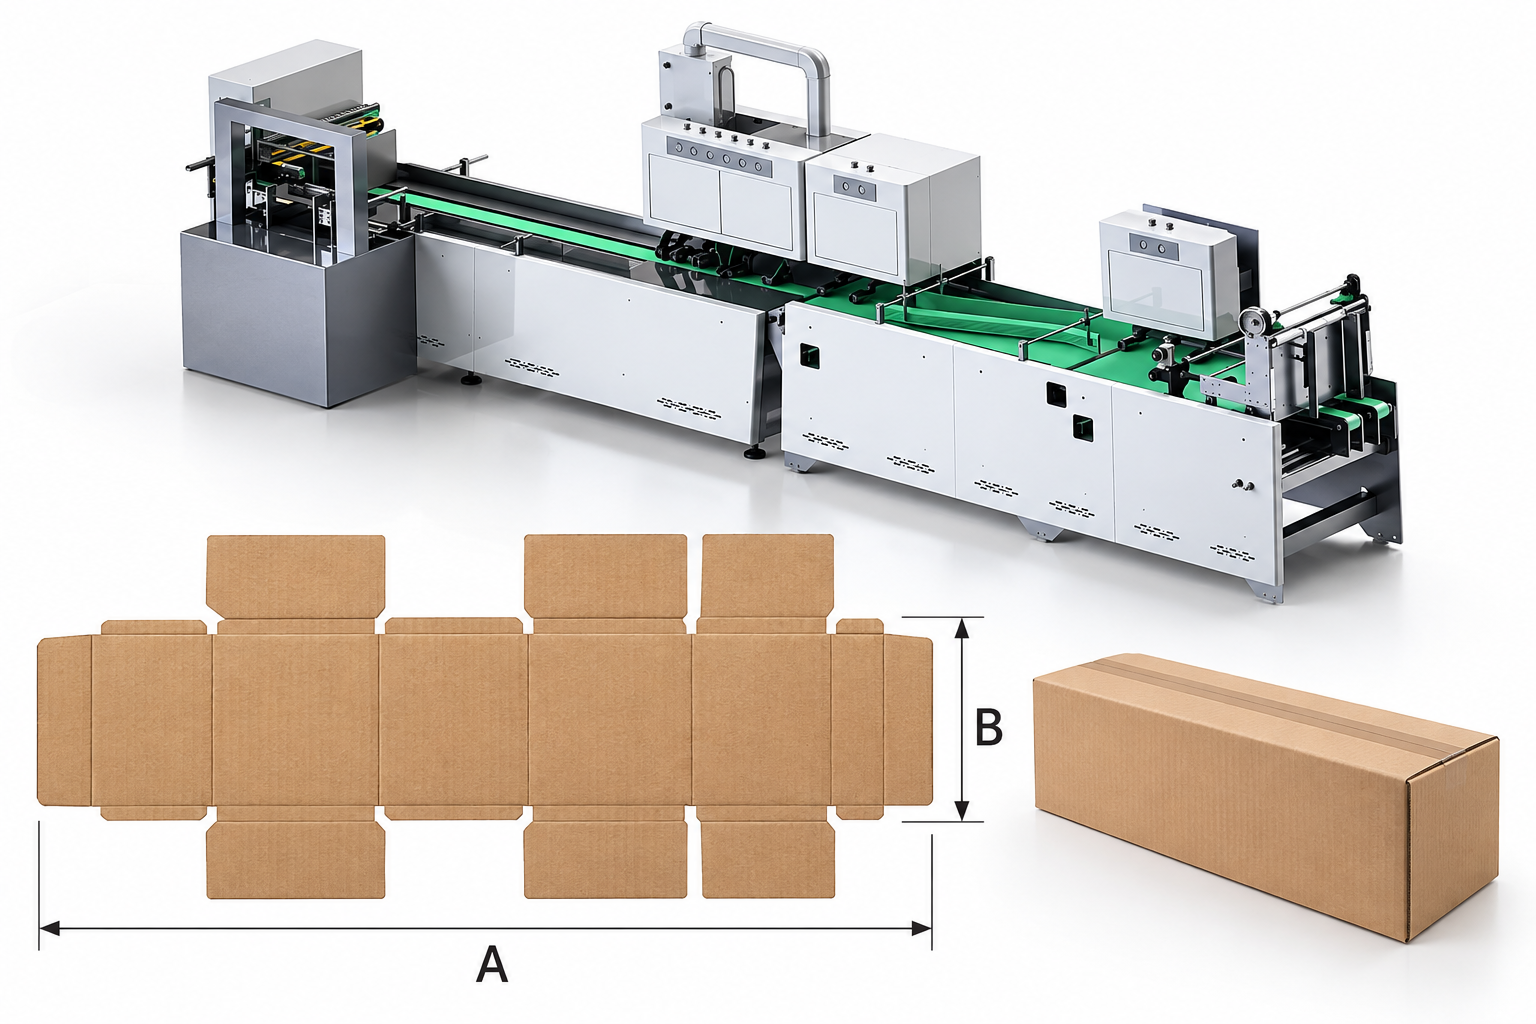
Drawing of a flattened straight-line corrugated box with dimension A along its length and dimension B across its width
A is the length and B the width of the flattened box.
How A, B and Stack Height Are Measured
A is the length of the glued, flattened box and B its width; horizontal stacking needs A longer than B.
Stack height is measured uncompressed, before the strap goes on.
Measure your caliper by ISO 3034, the ISO method for the single sheet thickness of corrugated fibreboard.2
Calculation Formula
Boxes per bundle = stack height ÷ (2 × board caliper)* Because a flattened box is two board layers thick.
Stacking Modes and Folder Gluer Line Configurations
Where boxes are folded and glued, the flat box is thicker. If the flattened boxes are simply piled one on top of the other, the pile soon leans into an unstable wedge, so piling them up does not necessarily give a stable bundle.4
On lines without automatic stacking, an operator below the counting machine rotates or flips half-bundles by hand before strapping.4
Here the pusher rod and flip plate build each stack in one of two modes, vertically or horizontally, based on the box size you provide.
Configuration Specifications
| Configuration | What it does | Choose it when | Supplied by |
|---|---|---|---|
| Horizontal stacking, horizontal push | Stacks the boxes horizontally and pushes the stack into the strapping unit | Your flattened box is A 200–360 mm and B 120–290 mm with A longer than B, and the stack is 230–550 mm uncompressed | Cenwan |
| Vertical stacking, horizontal push | Stacks the boxes vertically and pushes the stack into the strapping unit | Your flattened box is A 300–550 mm and B 200–450 mm, and the stack is up to 400 mm uncompressed | Cenwan |
| Retrofit behind your folder gluer | Runs inline after your existing straight-line, automatic folder gluer or flexo folder gluer (FFG) | You want to upgrade a folder gluer line you already run; we confirm the integration with your folder gluer model in the quotation | Cenwan machine, your folder gluer |
| Inside a Cenwan line | Closes a dual-channel folder gluer line or a printing, die-cutting and folding gluing line | You are buying the line and want one supplier from flexo printing to strapped bundle | Cenwan |
System Integration & Output
Stack height in both modes is set by your board caliper (ISO 3034) and the count per bundle your customers order. Standalone machines and integrated lines are both part of our automatic packaging line range; paired with a folder gluer, these rear-end packaging machines further increase overall productivity and reduce dependence on labor.
Corrugated Box Strapping Machine Specifications
The following are all specifications for the machine. The rate that you achieve on your line is dependent on box length, count per bundle and your folder gluer’s delivery.
Horizontal-vs-Vertical Stack Size Limits
Price, Lead Time and Payment Terms
The price is set by the stacking mode, your box size range, whether the machine stands alone behind your folder gluer or joins a Cenwan line, FOB Wenzhou or EXW terms, installation engineer-days and whether you need expedited production. There is no fixed price list; your figure comes back in a written quotation.
Price Variables & Configuration
Stacking mode
Effect on price
The mode follows your box size range
Action Required
Send the full range once, so one mode covers it
Standalone vs Line
Effect on price
A line adds the machinery upstream of this one
Action Required
Buy the tail end alone if your folder gluer stays
Connection to Folder Gluer
Effect on price
Your model and delivery height set the infeed work
Action Required
Send model, delivery direction and height with your enquiry
Trade Terms & Installation
Effect on price
FOB Wenzhou or EXW, plus engineer-days on site
Action Required
Plan your site power and air before the engineer arrives
Production Schedules
30–45
Business Days
Standalone machine
Production of the machine
45–60
Business Days
Integrated line
Production of the whole line
Rush Order
Expedited
Expedited Production
Requested at quote stage and confirmed with your deposit
48H
How Your Quotation Is Produced
Quotations are returned within 48 hours of receiving your box specification: flattened box size range, flute, count per bundle, folder gluer model and line speed. An engineer checks the stacking mode and the connection before the price is set.
Payment is a 30% T/T deposit with 70% before shipment, and L/C is accepted. We quote FOB Wenzhou or EXW.
Work Out Payback on the Investment With Your Own Numbers
Payback months = delivered cost ÷ ((people moved off the delivery end × shifts × hours × working days × loaded hourly cost − added running cost) ÷ 12)
Open Payback Worksheet ➔
Quality Assurance: Factory Acceptance Test & Support
Every machine runs a factory acceptance test before shipment as its final quality control step, against acceptance criteria agreed in your contract. A third-party pre-shipment inspection can be arranged on request.
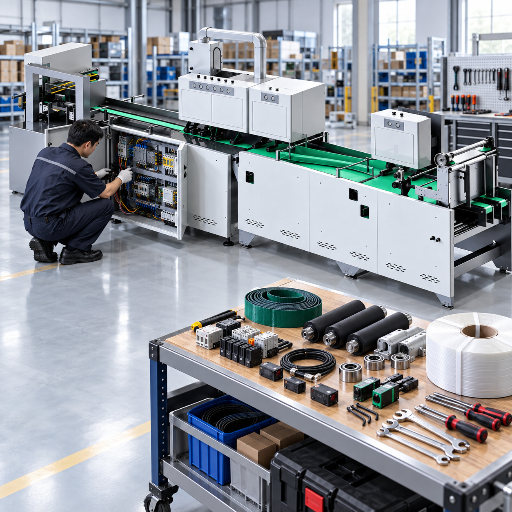
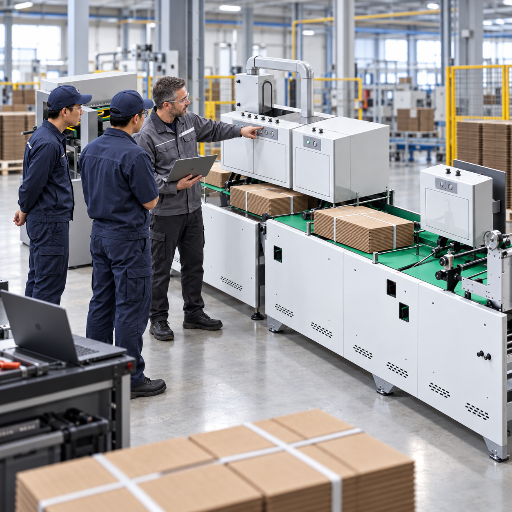
How We Work: From Box Specification to First Strapped Bundle
Step 01
Send your box data
Range of flattened box size, flute, count per bundle, folder gluer model and line speed.
Step 02
Quotation
Returned within 48 hours, with the stacking mode and the connection to your folder gluer confirmed.
Step 03
Deposit and production
30% T/T deposit, then 30–45 business days of production for a standalone machine.
Step 04
Factory acceptance test
The machine runs against the acceptance criteria in your contract before shipment.
Step 05
Shipment
FOB Wenzhou or EXW, after the 70% balance.
Step 06
Installation and training
Our engineer will require 3–5 days to install the machine and provide training to your operators; strapped bundles then go to your pallet either manually or through a palletizer you add.
Data We Need From You
Folder gluer brand and model
Sets the infeed and how the two machines share the delivery
Delivery direction and height
Places the machine in line with your compression section
Line speed (m/min) or boxes per hour
Checks your rate against the 18,000–30,000 pcs/h rating
Smallest and largest flattened box (A × B)
Chooses horizontal or vertical stacking
Count per bundle
Sets stack height against the stack limits
Voltage, frequency and air supply
Matches the electrical cabinet and pneumatics to your plant
Core Modules
Auto Strapping Arch
Integrated strapping mechanism ensuring seamless, continuous box flow without jamming or manual interference.
Double Channel Design
Maximizes output by processing two streams of cartons simultaneously, doubling the efficiency of single-channel systems.
Servo Paper Separation
Utilizes dual belt sets driven by advanced servo motors for clean, instantaneous batch separation.
Laser Displacement Sensor
Works in tandem with the counting roller to provide highly accurate, zero-error carton counting at high speeds.
When a Counter Ejector and a Separate Strapper Fit Better
An integrated machine may not always be the best choice as a tail end solution. If your high-speed flexo folder gluer already delivers counted stacks through its own counter ejector, adding one of the standalone automatic strapping machines built for corrugated bundles is the smaller step, and the modular pair keeps a conveyor between counting and strapping.
Solution Comparison Data
| Steps & Features | Integrated counting, stacking and strapping machine | Counter ejector + standalone strapping machine | Manual counting + semi-automatic strapping machine |
|---|---|---|---|
| Steps covered | Count, separate, stack, strap | Count and stack; strap on a second machine | Strap only; people count and stack |
| Machines to install | One | Two, plus the conveyor between them | One strapper |
| Control hand-off points | Inside one PLC | Between two machines | Between people and the strapper |
| What one stoppage affects | Downtime of one step stops counting, stacking and strapping together | The conveyor between them holds stacks while a jam in one machine is cleared | Hand work continues while the strapper is cleared |
| Hands still needed at the end of line | Moving strapped bundles to the pallet | Moving strapped bundles to the pallet | Counting, stacking and feeding the strapper |
| Strap | PP (polypropylene) strap | PP or PET (polyester), to suit the strapper | PP or PET (polyester), to suit the strapper |
Alternative Configurations
Operational Trade-offs
The trade-off is floor space and hand-offs against one control system. When the answer is not this machine, here is where to look instead.
| Situation | Why it works against you | What to do instead |
|---|---|---|
| Your folder gluer already has a counter ejector | Counting and stacking are already automated | Add a standalone strapping machine after the counter ejector |
| Lock-bottom boxes | Outside our range: this machine takes straight-line boxes | Send the box style and we will reply with the options |
| 4-corner or 6-corner trays | Outside our range: not straight-line boxes | See the 4/6 corner folder gluer |
| Stereo boxes, display boxes and paperboard folding cartons | Outside our range: not corrugated straight-line boxes | See the stereo box folder gluer |
| Flattened boxes longer than 550 mm | Beyond both stacking modes | Send the size; we will say what the line can take |
| Folder gluer output below 18,000 pcs/h | Your line runs below the 18,000–30,000 pcs/h rated band | Run the Bundle-per-Minute Check or send your line speed and box sizes; we confirm the setup in your quotation |
Automation & Efficiency Calculators
Bundle-per-Minute Check
Enter what your folder gluer delivers and how many boxes you put in a bundle. The check converts your rate into bundles per minute, estimates the uncompressed stack height, and shows which stacking mode of the Cenwan carton counting, stacking and strapping machine fits your flattened box.
Access CalculatorBoxes-per-Bundle Range Finder
Enter your board caliper to discover the bundle capacity for each stacking mode on the Cenwan machine. Input your customer’s required bundle count, and the system will automatically match the optimal stacking mode.
Find Optimal RangeTail-End Automation Payback Calculator
Work out the ROI and payback period of automating counting, stacking and strapping at your folder gluer delivery end. Enter your own headcount, wages, and delivered price below.
Calculate ROICounting, Stacking and Strapping Machine FAQs
How does an automatic carton counting and stacking machine count boxes?
A roller rides over the shingled boxes and a laser displacement sensor reads its rise and fall; each peak and valley is one box. Before the count, a two-stage feed pulls overlapped boxes apart with a belt speed difference.
Can the machine connect to my existing folder gluer?
Yes, it takes the delivery of a folder gluer to build a fully automatic line. Send your folder gluer model, delivery direction and top line speed, and we confirm the connection in the quotation.
Which corrugated board grades and box sizes does it handle?
B, C, E, BE, N and F flute straight-line boxes. Horizontal stacking takes flattened boxes A 200–360 mm by B 120–290 mm; vertical stacking takes A 300–550 mm by B 200–450 mm.
How fast can it count and stack corrugated boxes?
The rated packing speed is 18,000–30,000 pcs/h, with 30,000 pcs/h as the maximum, so a high speed folder gluer delivering more than 30,000 pcs/h is beyond this machine. Your rate depends on box length, count per bundle and your folder gluer’s delivery; the Bundle-per-Minute Check turns your numbers into bundles per minute.
What is the difference between a counter ejector and an integrated machine?
A counter ejector is a counting machine that stacks and ejects the count, and a second machine, typically a fully automatic strapping machine, straps it. An integrated machine counts, separates, stacks and straps all under one PLC. This results in the installation of a single machine instead of two.
Will the PP strap we buy now run on this machine?
Strap width, coil core and straps per bundle are confirmed in your quotation. Order polypropylene strapping for the machine it feeds, not by material and width alone.
What determines the price of a corrugated box strapping machine?
Stacking mode, box size range, standalone or line, trade terms and installation days. Quotations are returned within 48 hours of your box specification; payment is a 30% T/T deposit and 70% before shipment, FOB Wenzhou or EXW.
What is the lead time and how is installation handled?
Production takes 30–45 business days for a standalone machine and 45–60 business days for an integrated line. Our engineer installs a standalone machine in 3–5 days; you cover visa, airfare and lodging plus USD 150 per engineer-day.
What warranty and spare-parts support is included?
A 12-month warranty from the delivery date covers the electrical components in the control cabinet, with lifetime spare-parts supply. Lifetime remote video support runs by WhatsApp and video in English or Mandarin, with 24h emergency response.
How does the machine prevent short counts and overlapped boxes?
The two-stage feed separates overlapped boxes before counting, and the count check is an acceptance criterion in your contract, run at the factory acceptance test. Count reliability also depends on a clean sensor: dirt, dust and paper fibre on the sensor window affect laser readings, so keep the window clean as part of your daily routine.