Get in touch with Cenwan Machine Company

How to Qualify a Digital Print-to-Carton Line Retrofit

A digital printing packaging line retrofit for corrugated cartons starts by asking, what leaves the press? What happens before a finished box is accepted? Digital presses can produce printed sheets. Cutting, creasing, folding, gluing and stacking still require equipment, space, and ownership of the control system. Use this guide to evaluate four alternative layouts for the same set of jobs and acceptance tests that were selected by the buyer.
The scope in this case is corrugated board converted to cartons. Flexible packaging film, pouches and product-filling lines have different interfaces. Digital printers serve many parts of the printing industry; within the packaging industry, carton design defines which converting steps are needed. Cenwan’s published printing, die-cutting, folding and gluing line describes an integrated offering which includes an optional flexographic printing unit. That page doesn’t describe compatibility with any digital press. Ask for a model-specific interface study and a witnessed trial before putting any combined-line claim in a purchase order.
1. Draw the route from printed sheet to accepted carton
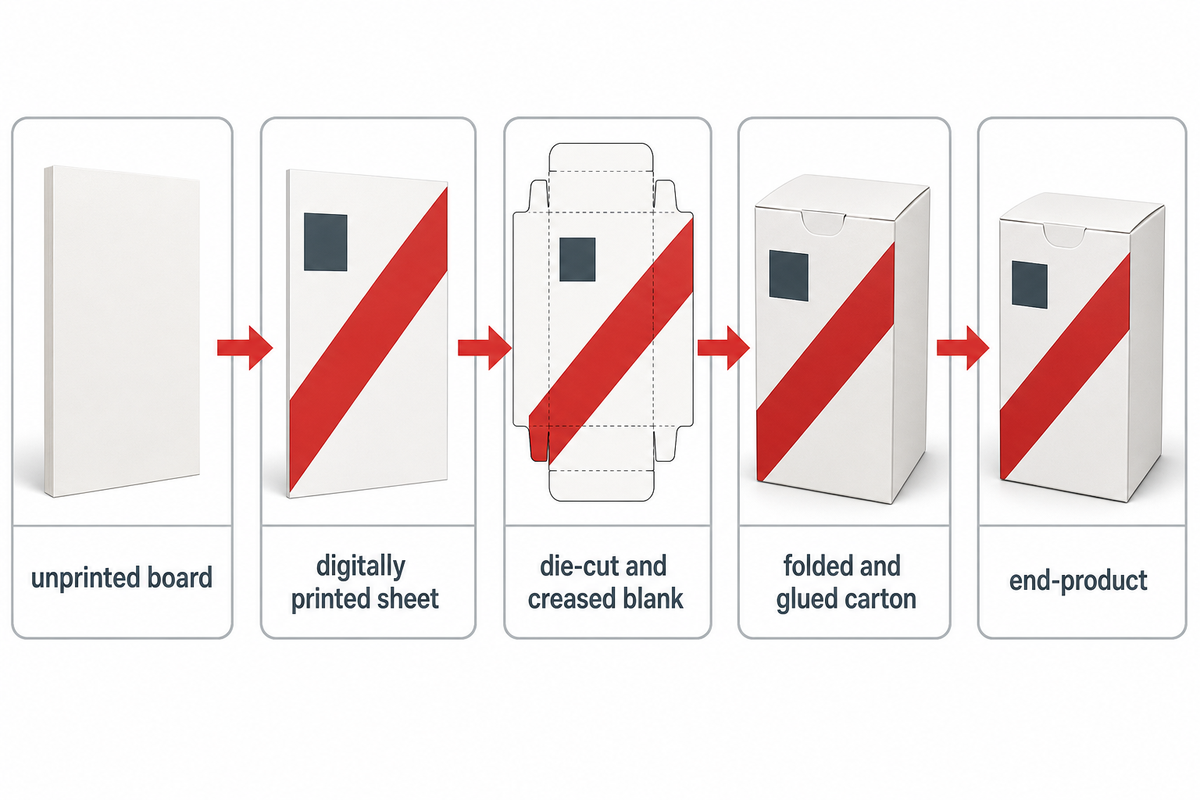
A retrofit from a press to cartons connects more than two frames. The buyer needs to identify all the changes in form of the product, i.e., unprinted board, digitally printed sheet, die-cut and creased blank, folded and glued carton, and end-product. FEFCO’s production description identifies printing, die cutting, folding and gluing as converting processes. It describes die cutting as cutting and creasing the board. The processes may be done on different machines or in combined equipment. Therefore, a press specification can’t be a surrogate for the end-to-end process.
Draw the actual plant layout, identify the owners of the feeder, discharge, drying or curing, cutting and waste removal, turner, gluer infeed, counter and stacker. For each handoff, document the size, orientation and height of the sheet or blanks, the condition of the stack, and the allowed state of stoppage. The Domino X630i product page, for instance, presents a digital corrugated press containing a feeder, vacuum transport, dryer and a stacking or bundling unit. This is an example of a printed-sheet system, not evidence that this press fits Cenwan equipment.
Purchase drawings should show mass balance from press sheets to usable blanks to first-pass acceptable cartons. If the press outputs a sheet and the folder gluer takes a creased blank, put the die cutter and its scrap stream on the drawing. A digital printing solution in the printing system changes image formation; it doesn’t omit the blank making stage from packaging production lines. Digital printing technology alone doesn’t define the finished-carton rate. Cenwan’s automatic line overview can give a general idea of modules to the buyer; it isn’t a digital press control interface.
Decision point: Ask each supplier to mark the last product they warrant and the first product the next supplier accepts. A signed drawing is stronger than a brochure photograph of machines placed side by side.
7-Check Press-to-Carton Interface Worksheet
- Press discharge: sheet size, height and orientation.
- Printed surface: drying, scuff and glue-area condition.
- Die cutting: registration, crease and waste removal.
- Blank transfer: turn, stack and separation limits.
- Gluer infeed: caliper, flap position and feed stability.
- Controls: job identity, blocked/starved states and restart.
- Finished output: first-pass packable cartons and reject trace.
2. Select the jobs before comparing machines
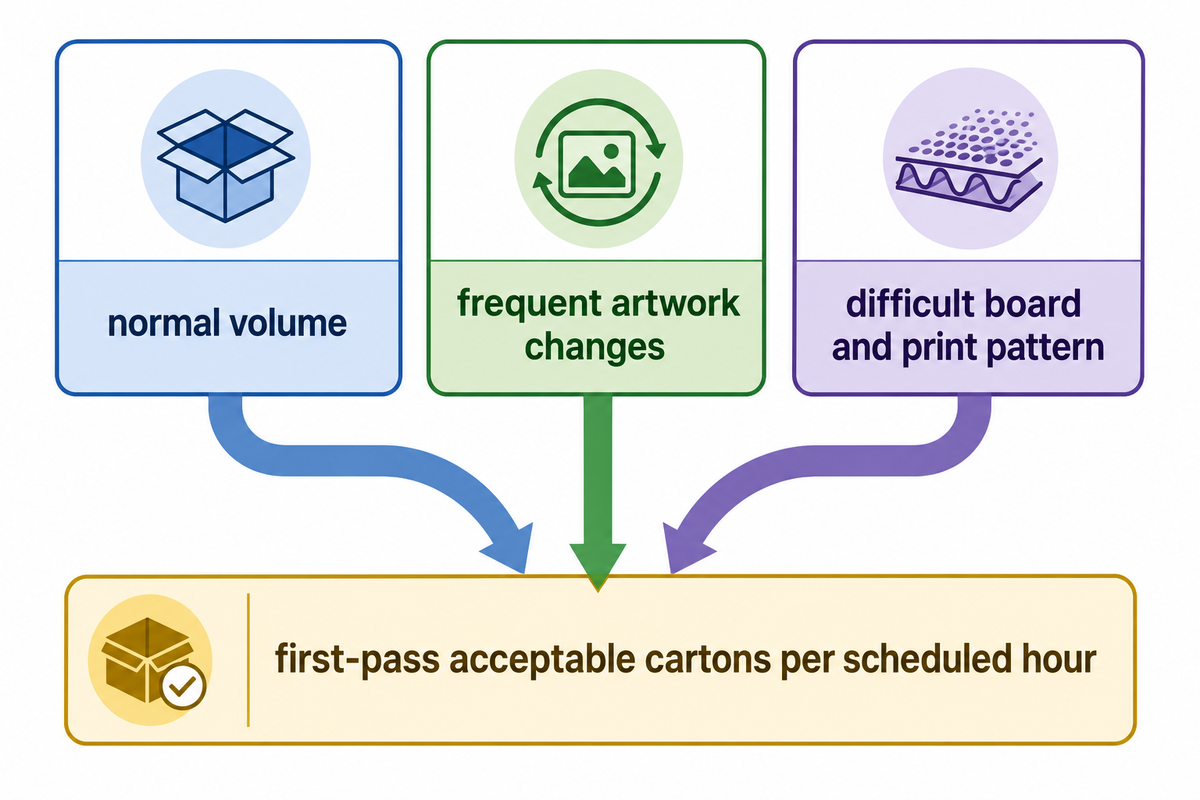
Choose representative corrugated jobs and compare the sheets per hour of the press to the belt speed of the folder gluer. One job should be of a normal volume and the other of frequent artwork changes. A third job should be of difficult board and print pattern. For each of these proposed layouts, log the style, dimensions and run length of the carton. The benchmark should be first-pass acceptable cartons per scheduled hour, not best minutes during a demonstration.
For each sample, fill in flute, board grade and caliper, sheet dimensions, print coverage, ink or coating, crease pattern, glue-flap location, and pack specification. Indicate the kraft liner if it’s part of the actual substrate, and indicate the CMYK or spot-ink recipe if it changes the print quality or drying. Keep the samples provided by the buyer for the current line. If the new digital job uses a different ink or board source, that’s a separate trial condition. See the board comparison guide for terminology. The qualification record, however, requires measured samples from the buyer’s orders.
How does a corrugated digital printing machine reduce costs?
Traditional printing methods may require printing plates and plate-making for each artwork set. A plate-free digital press can remove plate-making within pre-press on short production runs, but mechanical setup still occurs. Variable data or customization can change the value of custom packaging without changing carton geometry.
Costs will vary based on how frequently artwork changes, how many acceptable cartons survive finishing, and whether freed time is sold or labor is redeployed. For the current and the proposed method, put the relevant tasks for the same job on the same job log. Record press setup, mechanical changeover, handling, rejects and scheduled time. Then, compare total costs of an accepted carton for the buyer’s real order mix.
A mechanically efficient route may favor a long job; multiple SKUs with frequent artwork changes may favor digital packaging, but may also expose gluer changeovers. Track turnaround from approved artwork to a first accepted carton, rather than from file upload to first printed sheet. That gap impacts the promise made to the customer in supply chain. Neither of these cases is a definitive answer for a plant without job logs. For the quotation: For the quotation, have suppliers cost the same three jobs and state which costs their scope doesn’t address.
3. Qualify the die-cut blank at the gluer infeed
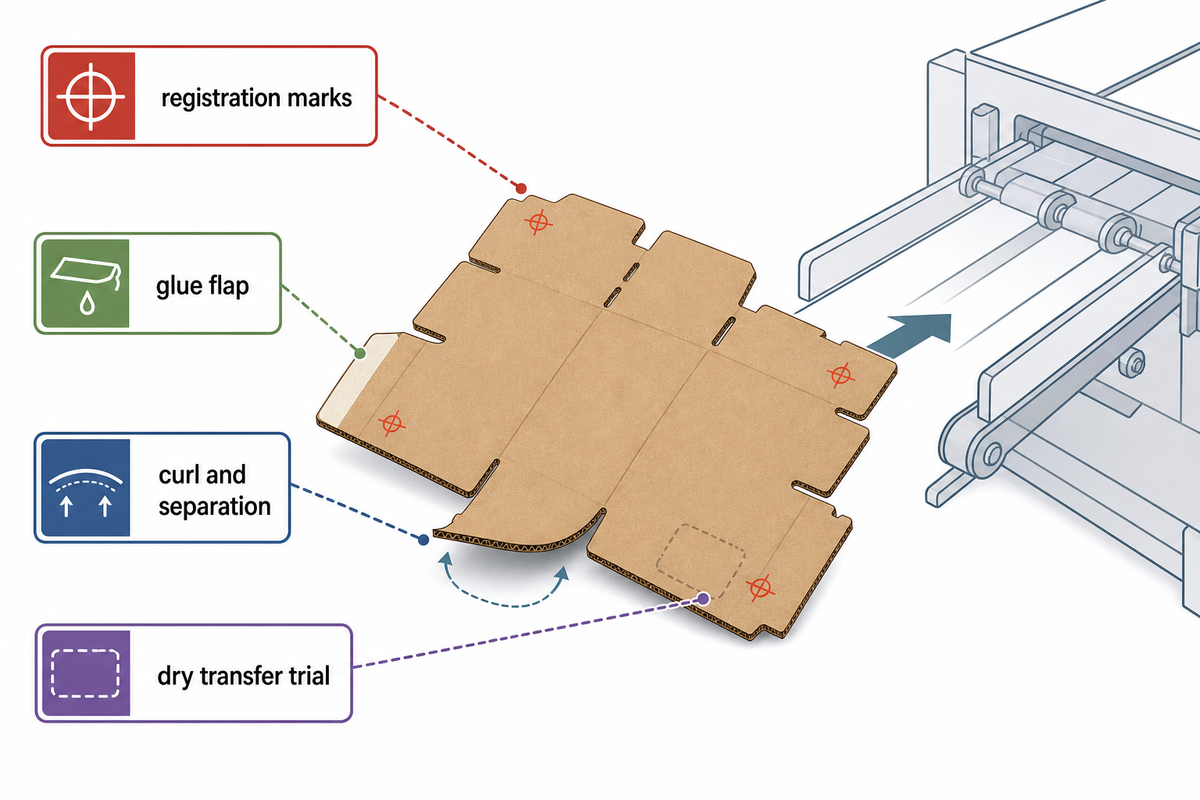
A digital-printed sheet is ready for folding and gluing only after the required cutting, creasing, and waste removal produce a blank within the gluer’s feed envelope. Inspect the actual infeed face, leading edge and the orientation of the glue flap. Confirm that registration marks survive the selected cutting route and that the flute direction and crease geometry are appropriate for the box style.
Measure blanks at the feed point rather than copy the press’s maximum sheet size into the gluer specification. Check the edge of die-cut sheets for squareness, curl and separation. Check caliper and skew of die-cut sheets. Ensure that margins and print, if any, are outside the glue area. Record the tolerance the buyer and machine suppliers agree to use; this article cannot supply a universal registration limit. A public patent on vacuum transport illustrates why holding sheets and exposed apertures are important for digital print transport, but that patent belongs to another company and proves no Cenwan feature.
A dry transfer trial is recommended at start up, steady running, a commanded stop, and restart. Keep rejected and accepted blanks separate. A turner or buffer should be tested using the worst allowed stack and smallest box. A mechanical fit on a single ideal board is too limiting to authorize the entire job mix. For the quotation: For the quotation, list qualified blank styles and measured limits at each handoff.
4. Compare four physical routes on one scorecard
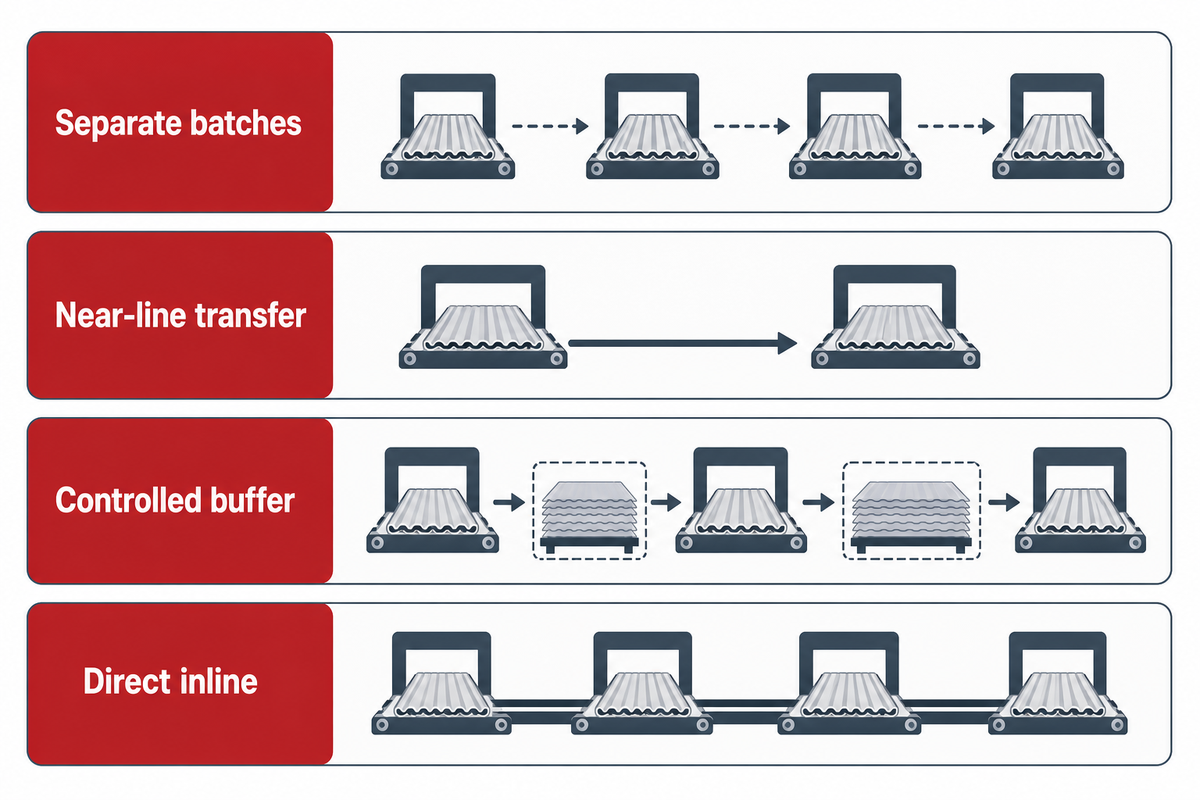
Separate, near-line, buffered and direct-inline routes address different types of issues in a digital production workflow. Direct connection can reduce handling, but a press stop may starve finishing and a gluer stop may block printing. Near-line routing provides more scheduling flexibility at the expense of additional moves and work in process. Buffers absorb small mismatches, and can’t raise a machine’s sustained capacity. Production environments with mixed orders may need routing flexibility that a direct-inline layout can’t give.
The OPC PackML state model differentiates between blocked and starved conditions. That terminology is helpful when writing acceptance log statements; it doesn’t mean that any named machine in Cenwan implements PackML. A 2025 trade interview on corrugated digital finishing also mentioned feeder, stacker and speed mismatch. Test these conditions on the buyer’s orders, instead of choosing a route based on appearance in the floor-plan.
| Route type | Works when | Watch closely | Acceptance proof |
|---|---|---|---|
| Separate batches | Different press and finishing schedules | Moves, mixed stacks, traceability | Batch ID through finished-carton count |
| Near-line transfer | Shared area with independent controls | Floor space and operator travel | Timed transfer and damage log |
| Controlled buffer | Short, measured stop or rate mismatch | Board marking, stack limits, FIFO | Full and empty buffer tests |
| Direct inline | Stable rate and matched jobs | Stop propagation and changeovers | Joint stop/restart trial |
| Press-side feeder | Reliable sheet singulation | Double feeds and curl | Recorded feed rejects |
| Print discharge | Dry, registered sheet exits | Scuff and orientation | Samples before conversion |
| Die-cut interface | Blank within measured envelope | Waste and crease variation | Measured first and last blanks |
| Gluer and stacker | Packable output is sustained | Adhesion, jams, bundle count | First-pass finished-carton tally |
| Staged decision | One interface remains unproven | Later controls and footprint cost | Written next-trial trigger |
Estimate buffer size with measured arrival and discharge rates, as well as the duration and frequency of stops, and the board’s safe accumulation limit. What happens when it’s full, empty or holds a combination of two different artwork? A buffer that holds damaged sheets or loses order identity creates packaging waste and another quality problem. For the quotation: Define the limit on how much can be allowed to accumulate, and who’s responsible for clearing a jam.
5. Count first-pass good cartons per scheduled hour
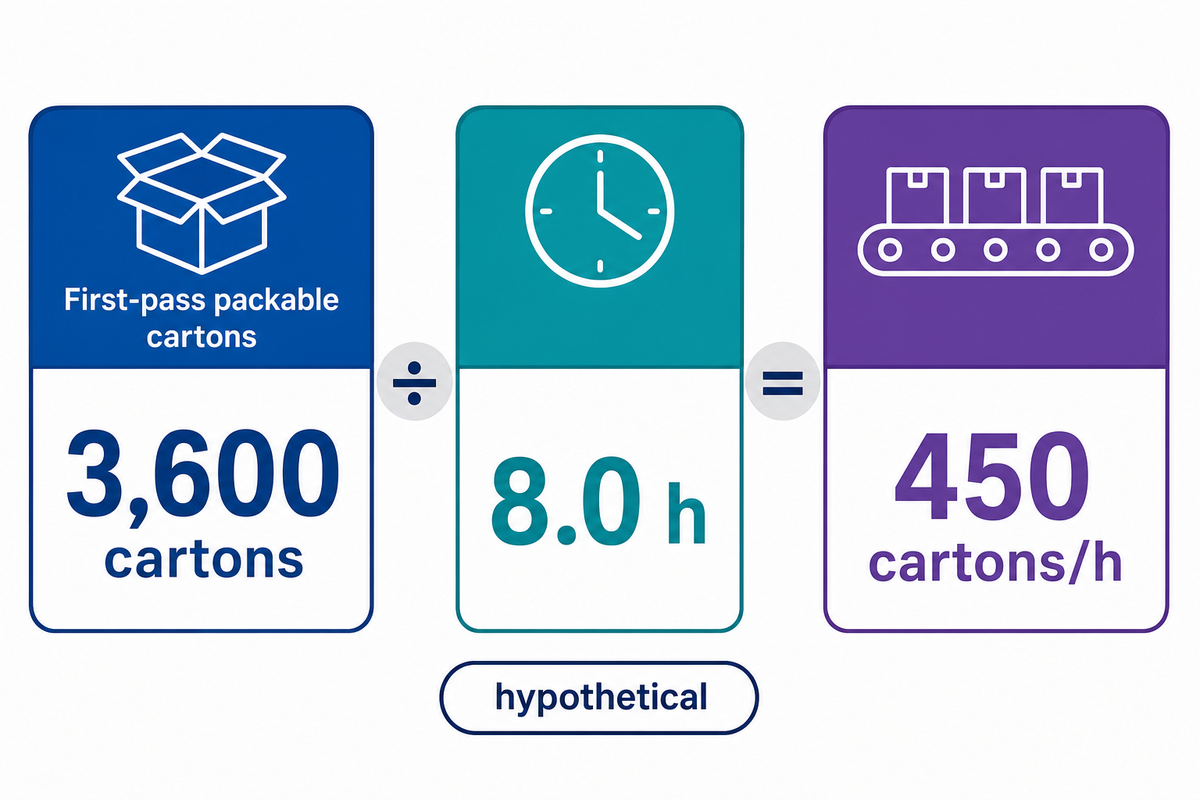
Use the same measure to evaluate all layouts. Use first-pass packable cartons divided by scheduled trial hours. In the denominator, include setup time and changeover. Exclude reworked cartons from the first-pass numerator, then report rework separately. Record print rejects, die-cut scrap, glue failures, jams and feeder or stacker stops by station. A supplier’s metres per minute or sheets per hour remains a useful machine specification, but it is not the same unit. High-volume production requirements still call for the same accepted-carton measure.
A published line page by Cenwan describes an ‘up to 240 m/min’ dual channel postal carton example. Domino’s X630i product page advertises up to 75 m/min (displayed there as ’75m/m’) or 4,500 sheets/hour for 900 × 1,500 mm sheets. These supplier claims relate to a converting line and a digital press in different conditions, and don’t represent a combined line carton rate. Obtain a format specific count and first-pass yield.
| Recorded item | Example input | How to use it |
|---|---|---|
| Scheduled trial window | 480 min | Denominator remains 8.0 h |
| Setup and two job changes | 55 min | Keep in scheduled time |
| Feeder and stacker stops | 28 min | Log by cause and owner |
| Blocked or starved transfer | 22 min | Test buffer claim |
| Restart and cleaning loss | 15 min | Count before steady run |
| Printed sheets presented | 4,200 sheets | Input count only |
| Conversion rejects | 240 cartons | Separate die-cut and glue causes |
| First-pass packable cartons | 3,600 cartons | Numerator |
| Comparable output | 450 cartons/h | 3,600 ÷ 8.0 scheduled h |
This example assumes that one carton corresponds to one counted blank, and that there’s no multi-up layout. Change the sheet-to-carton conversion if the buyer’s die layout is different. Perform this analysis for the current system and the alternative configurations, using matched jobs and shift boundaries. Don’t assume that 450 cartons/hour represents a supplier guarantee. A temporary buffer may help in alleviating 22 minutes of blocking or starvation. It, however, can’t help in addressing a persistent bottleneck after it fills.
Hidden Bottleneck Map
| Observed symptom | Likely station to test | Buyer proof |
|---|---|---|
| Printed sheets queue | Die cutter or transfer | Arrival/discharge count by job |
| Blank stacks wait | Gluer infeed or changeover | Start-to-first-good timeline |
| Gluer waits for sheets | Press feeder, print or discharge | Starved-state log |
| Whole route stops | Coupled controls or full buffer | Blocked-state and restart log |
| Output looks high but cartons fail | Print, crease or adhesive joint | First-pass reject tally by cause |
This map is a sample production plan, NOT a diagnosis of Cenwan or a buyer plant. The best practice is to use the first station that repeatedly constrains the flow of work to identify potential options for capacity or decoupling.
Which businesses benefit most from a digital printer for corrugated boxes?
Frequent changes to artwork, small batch sizes or products with variation may be better supported with plate-free printing, as long as the finishing processes are flexible enough to handle the variation. A converter that produces on-demand corrugated boxes for e-commerce, may prefer shorter lead times, but it’s the actual order mix that proves this preference. A converter that has long, stable runs, may prefer converting capacity. The answer should come from the job distribution and accepted-carton count. [NIST’s equipment-effectiveness case] provides a way to look at the equipment, processes, and people in a broader perspective to focus on improvement in terms of availability, performance, and quality. Their examples for metalworking processes aren’t benchmarks to the corrugated.
6. Test print durability and the finished glue joint separately
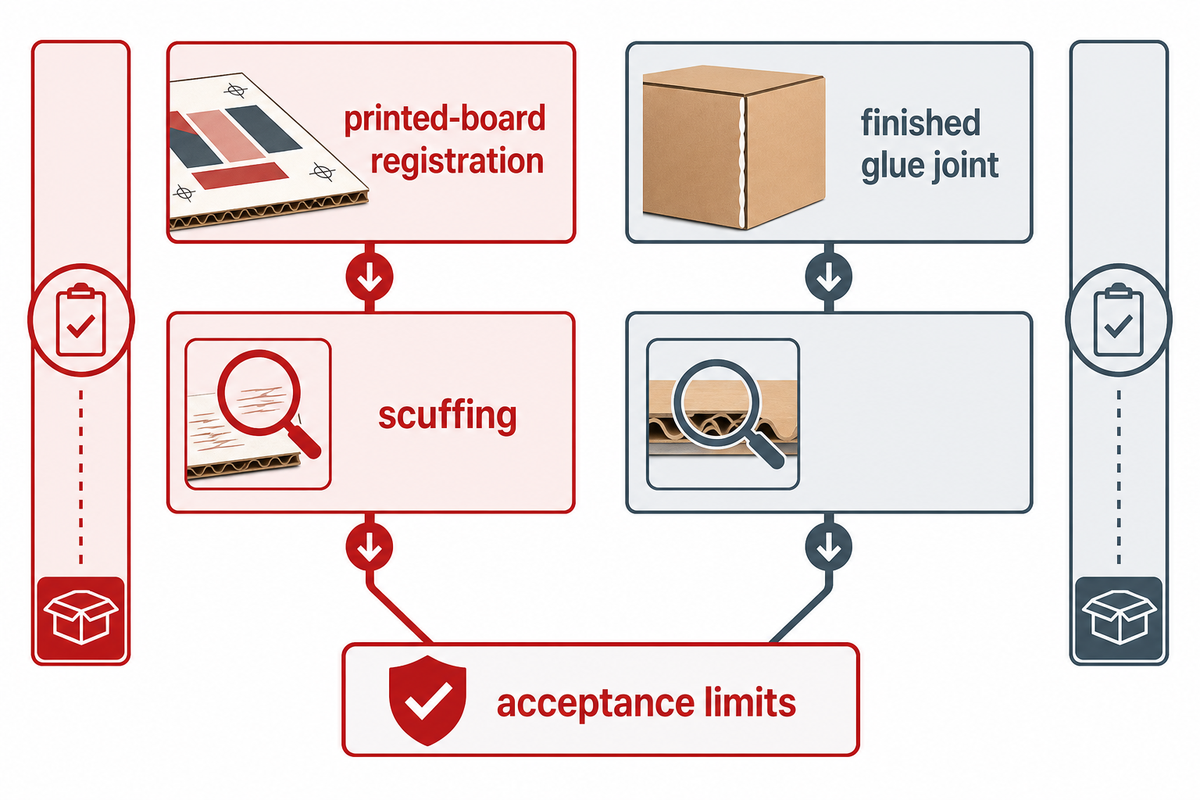
Two distinct quality paths are necessary to assess a shipping container. First inspect the printed-board registration, scuffing, cure or drying and crease cracking on the buyer’s board and ink. Inkjet print quality on custom printed corrugated boxes should be inspected prior to conversion; keep printed materials from both start up and run in. A sample may show quality printing while its finished glue joint fails. Then assess the alignment of folds, placement of glue, and the development of the bond at the joints of the finished cartons at the proposed speed. Good ink adhesion to a liner doesn’t assure a sound bond of the flap to the glue.
The historical TAPPI T 840 om-10 description refers to the testing of adhesives on laboratory prepared specimens and identifies T 813 as a different method for testing finished containers. TAPPI’s 2015 withdrawal notice states that T 840 om-10 was withdrawn. A buyer shouldn’t consider it as a current official method. Agree with the quality team on the applicable method, conditioning of the samples and acceptance limits prior to testing.
Keep all failed samples and indicate on which step of the process (printing, die cutting, fold alignment or gluing) each failure started. The corrugated box gluing guide provides a broader process context; the retrofit sign-off requires a sample record in its own right. One day’s successful bond shouldn’t erase a failure on a different board or a long storage interval. For the quotation, state who pays for repeat samples after a failed interface and attach the signed test plan.
7. Build a payback case from accepted output
Price the installed route, and then model the change in contribution from saleable cartons. Consider the digital or retained press, conversion equipment, transfer devices, controls, guarding, floor works, utilities, installation, training, and maintenance. Consider energy, consumables, board waste, and finance. Keep first-pass yield assumptions and demand assumptions visible. Some offers that are priced as packaging solutions at competitive prices still require an installed price and an acceptance scope. A packaging market average can’t price this site. NIST’s capital-investment guidance is helpful when considering discounted cash flows and sensitivity analysis; however, it doesn’t provide a universal retrofit return.
One approach begins with cartons that the plant currently accepts, proposed accepted cartons, and the orders the plant can actually sell. Multiply only the incremental saleable cartons by their contribution margin, then subtract incremental operating costs. Count a labor saving only if hours or headcount can genuinely be redeployed or avoided. Don’t count the same hour twice; once as a labor saving and again as extra plant capacity. A lease payment is a cash outflow and shouldn’t be used as evidence of payback. Competitiveness and market share should be tested at a later date; they aren’t revenues to include in this worksheet.
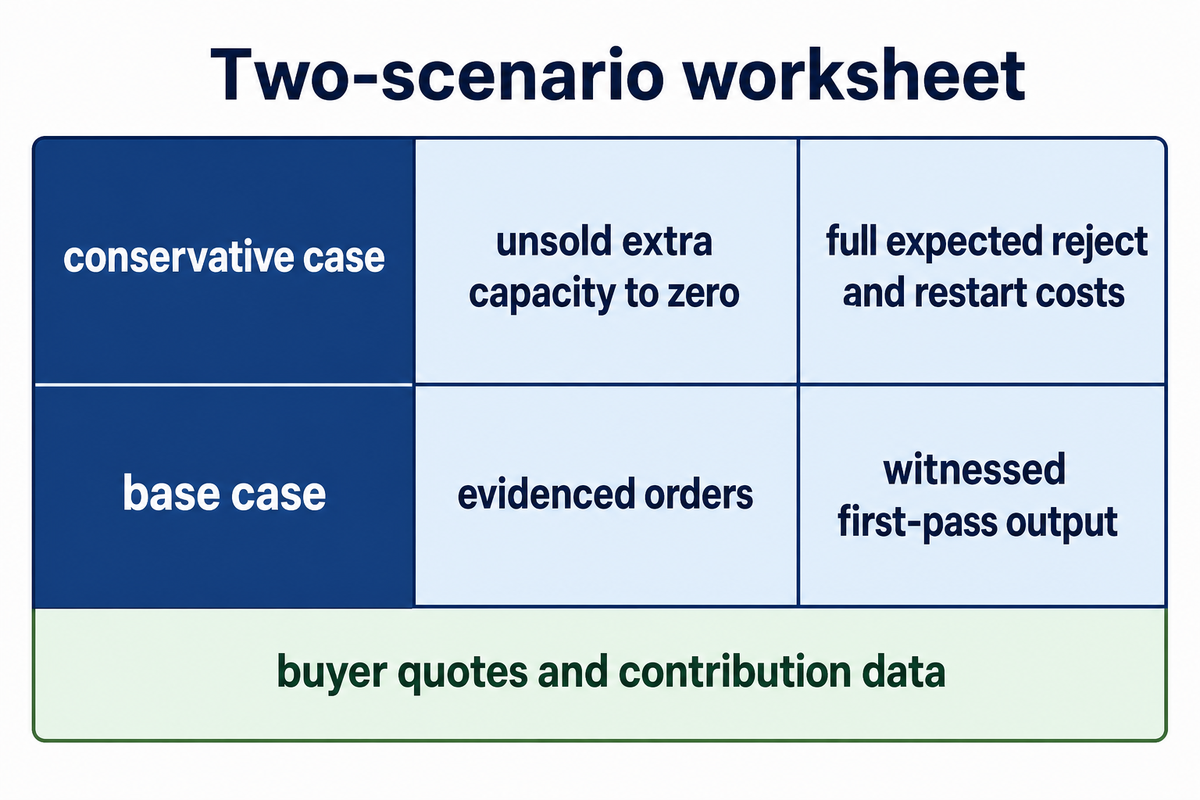
Two-scenario worksheet: The conservative case sets unsold extra capacity to zero and includes the full expected reject and restart costs. The base case uses evidenced orders and witnessed first-pass output. Both cases require buyer quotes and contribution data. No monetary result is asserted here because those inputs have not been supplied.
Ask suppliers to divide their quote into the equipment and interface work they own. A cheaper machine can lead to a higher installed price if controls and guarding are added or a missing die-cut stage is included later. The folder-gluer maintenance checklist provides a list of service tasks to price. For the quotation: For the quotation, list exclusions beside the prices, including test boards, software modifications, and on-site commissioning days.
8. Put an owner beside every interface
Each retrofit contract has a named owner for a product handoff, control action, and a safety function. Named warranties for a press and folder gluer don’t explain who resolves a blocked transfer or a disagreement on an emergency stop. Issue an interface schedule before placing an order and include it in factory and site acceptance tests. Determine which controls bear the approved artwork marker along the line.
| Interface | Named owner to fill | Acceptance evidence |
|---|---|---|
| Sheet discharge and orientation | Press supplier / integrator | Measured sample and drawing |
| Die-cut blank specification | Converter supplier | Approved blank measurements |
| Feeder, transfer and buffer | Integrator | Full/empty and jam tests |
| Job recipe and artwork identity | Controls owner | Mixed-job prevention test |
| Blocked/starved signals | Controls owner | State and restart log |
| Reject count and traceability | Quality / controls owner | Reconciled batch tally |
| Guarding and emergency stop | Safety lead | Risk review and witnessed test |
| Utilities and site layout | Buyer / installation lead | As-built survey |
| Commissioning and service | Contract lead | Signed limits and response terms |
“The person constituting an assembly of machinery is considered as the manufacturer of the assembly of machinery.”
That UK guidance applies to an assembly under its stated conditions. Identify the proposed assembly manufacturer and assess the actual line, jurisdiction and modification prior to assigning duties for the technical file and the declaration of conformity. The public ISO 12643-4:2023 page describes safety scope for converting equipment and systems; it does not establish this installation’s compliance. Public scope excludes machinery or components manufactured before publication; an existing machine retrofit therefore requires an applicability review. Insist the competent safety lead define applicable requirements and evidence in the contract.
How quickly can a carton packaging line switch between different product SKUs?
Report artwork change, mechanical setup and time to the first accepted carton separately. An electronic file switch may be quick, but different folds or dies, and glue positions require time. On the trial, start the clock on the last good carton of the job and stop the clock when the first good carton is accepted. Repeat for the three chosen jobs; use the changeover guide for a broader setup checklist.
9. Run a mixed-job go, stage or stop trial
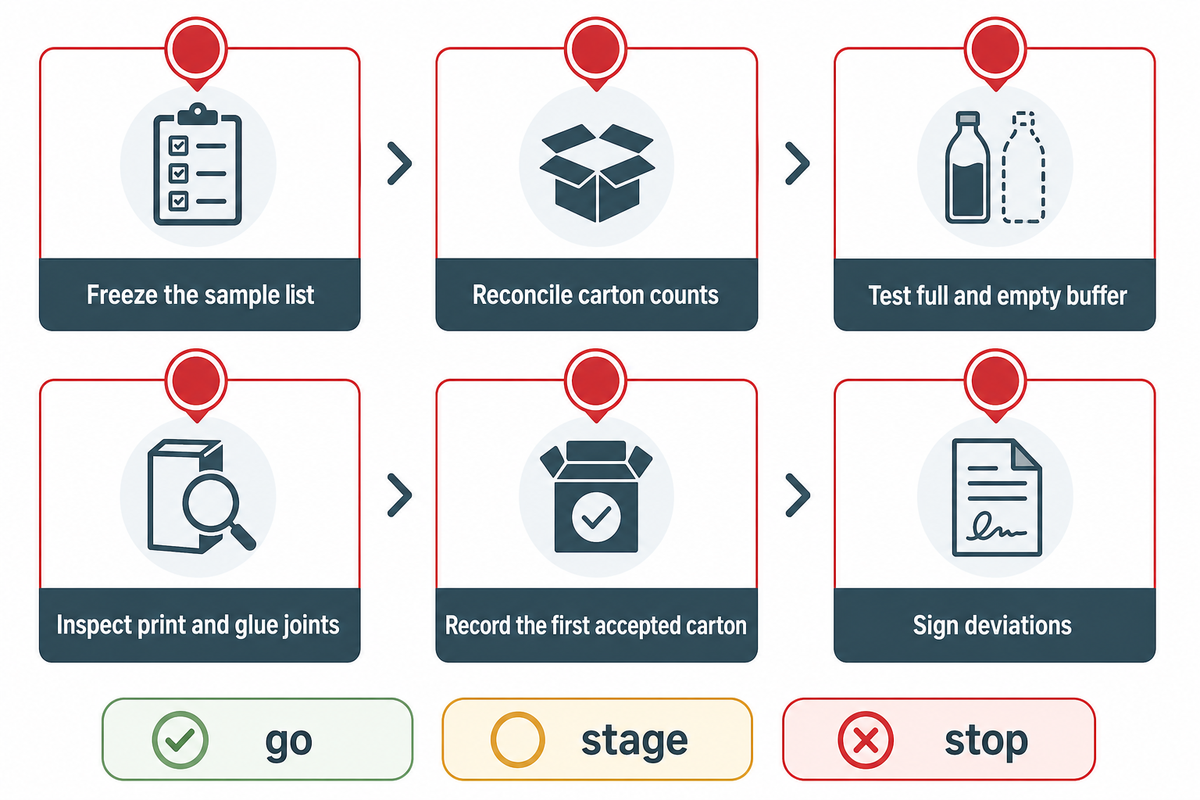
A witnessed test should reveal interfaces that fail when the job mix changes. Run the buyer’s normal, artwork-heavy and difficult board jobs in the planned sequence. Give every route the same scheduled definition and count first-pass packable cartons. Record each stop, its station, duration, recovery action and rejected material. Agree tolerances and the party signing each result prior to the commencement of the test.
- Freeze the sample list, artwork versions, board source, adhesive and acceptance limits.
- Verify finished-carton counts, die-cut blanks and printed sheets reconcile.
- Test full and empty buffer conditions, jam clearing, emergency stops and controlled restarts.
- Inspect registration, scuff, crease, folds and glue joints at startup and at a steady rate.
- Change jobs without clearing the loss log; record the first accepted carton after each job change.
- Sign deviations, corrective actions and a repeat-test condition if a critical interface fails.
Choose “go” when the agreed jobs and output are passing and the safety checks are cleared. Choose “stage” when a separate or buffered route is working, but a direct connection hasn’t been proven; write the missing test into the next project gate. Choose “stop” when it isn’t possible to qualify the board, blank or safety interface within the agreed limits. This protects the buyer from assuming that a single peak speed demonstration is commissioning.
Bring the seven interface checks to a technical review. If you are evaluating Cenwan finishing equipment for a specific digital press, share the press model, three representative jobs and current line drawing. Request a SKU-specific interface discussion. Compatibility and output remain subject to a buyer-witnessed trial.
10. Leave room for the next press without buying a forecast
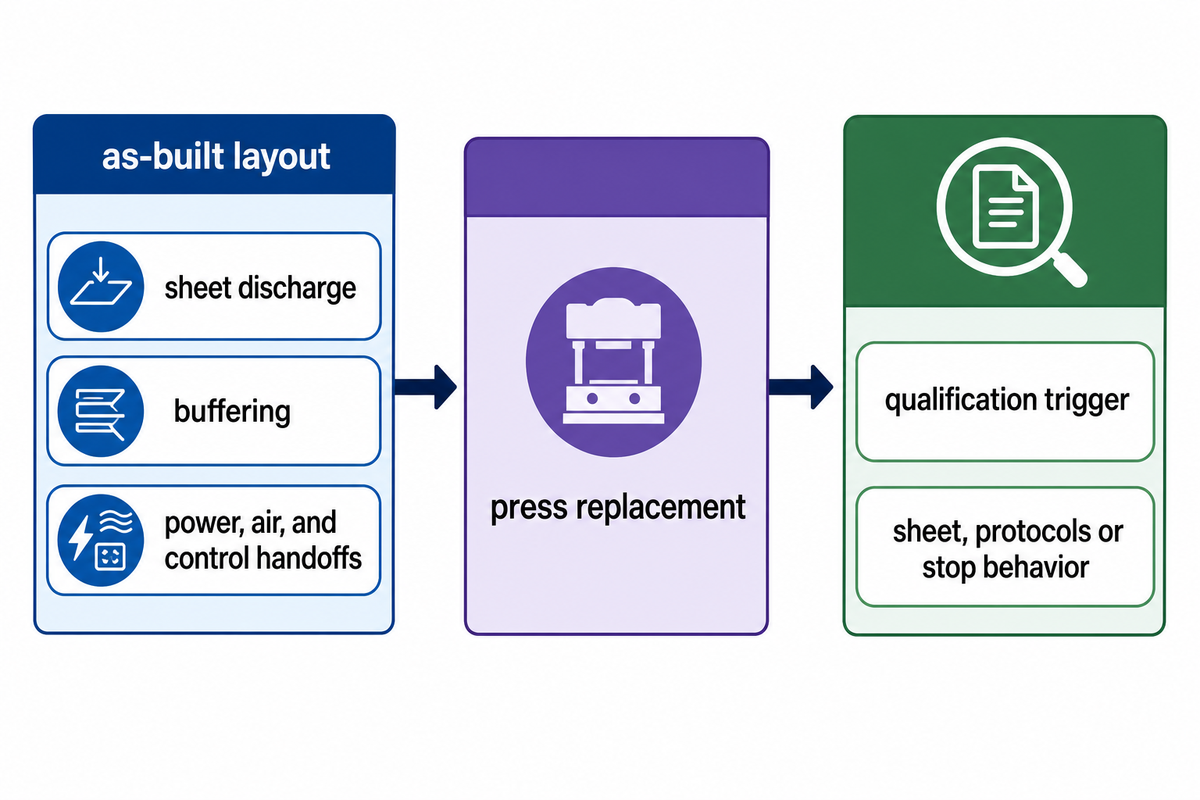
Retain the as-built layout and interface schedule to provide future flexibility. Maintain access to sheet discharge and buffering for turning, guarding, maintenance, and utility tie-ins. Record heights, orientations, power, air, and control handoffs. Ask how each would change if a different press were used. Document the current acceptance record; it may be needed if a press replacement is made. Don’t assume a new model press would use the same sheet, protocols or stop behavior.
Make the current job mix and acceptance the basis of investment. Future optionality for a press can be priced as a documented allowance with qualification trigger. For the quotation: require editable layout and interface drawings so the buyer can evaluate a later press without repeating the entire survey.
Frequently asked questions
How long does it take to put an automated carton line into full operation?
There’s no fixed lead time. Propose dates for the as-built survey, interface design, sample trials, factory acceptance, delivery, installation, safety review, and buyer-job commissioning. A schedule is believable when each step has a responsible party, input, and approval. A failed material or control trial has to state an interval to try again.
What does a digital printing machine cost?
A press quotation doesn’t price a press-to-carton retrofit. Request separate installed prices for the press, die cutting and creasing, transfer or buffer, folder gluer, controls, guarding, utilities and commissioning. Compare offers for first-pass accepted cartons and contract scope, using the same buyer jobs.
What is a digital corrugated printer?
It can print directly to corrugated board or sheets from digital image data. It can still require post drying, die cutting, creasing, folding and gluing to create a saleable carton. Ask for the actual format and orientation of the sheets as proposed by the vendor.
Can any digital press connect to an existing flexographic printing and gluing line?
No compatibility claim can be made from a general line brochure. To be qualified for the job, the chosen press’s sheet size, output height, orientation, drying, controls and sustained rate needs to be compared against the specific converting route, and then a buyer-job test is needed.
Is a buffer always required between printing and folding-gluing?
A buffer is useful when measured short stops or rate differences can be safely absorbed. Direct transfer can suit stable matched jobs; separate batches may suit independent schedules. Board-handling damage and a buffer’s size need to be evaluated.
References and sources
- FEFCO: corrugated production process, process boundaries.
- OPC Foundation: PackML state model, blocked and starved terminology.
- TAPPI: historical T 840 om-10 description and 2015 withdrawal notice; the historical page distinguishes lab specimens from finished containers.
- NIST: capital investment analysis, appraisal method.
- UK HSE. Machinery assembled in situ. UK-specific responsibility guidance.
- ISO 12643-4:2023 public page, published safety scope.
- Industrial Print Magazine: corrugated finishing interview, trade evidence on layout and handling.
- NIST: equipment-effectiveness case, measurement method only; its metalworking figures aren’t corrugated benchmarks.
Manufacturer Background
Cenwan Machine is a Wenzhou, China-based manufacturer of folder gluer machines, corrugated box gluing equipment, and integrated packaging lines. For more than 10 years, we have supported carton and corrugated packaging manufacturers in 40+ countries with equipment selection, custom configuration, installation support, spare parts, and after-sales service.
Our blog content is written to help packaging buyers, plant managers, and procurement teams understand folder gluer technology, box style compatibility, production capacity, ROI, maintenance, and supplier selection before requesting a quote.
- 10+ years of folder gluer engineering experience
- Factory base in Ruian, Wenzhou, Zhejiang, China
- Folder gluer machines, corrugated folder gluers, and automatic packaging lines
- CE / ISO 9001 manufacturing and quality references
- Remote diagnostics, spare parts support, and 24/7 technical response
- Equipment and service experience across 40+ countries
Brand
Cenwan Machine
Company
Zhejiang Chengwang Intelligent Packaging Equipment
Business Type
B2B Machinery Manufacturer
Factory Base
Ruian, Wenzhou, Zhejiang, China
Email
sales2@cenwanmachine.com
Phone / WhatsApp
+86 139 0664 6788